Explore performance details, construction highlights, applications, and technical information in one clear overview.
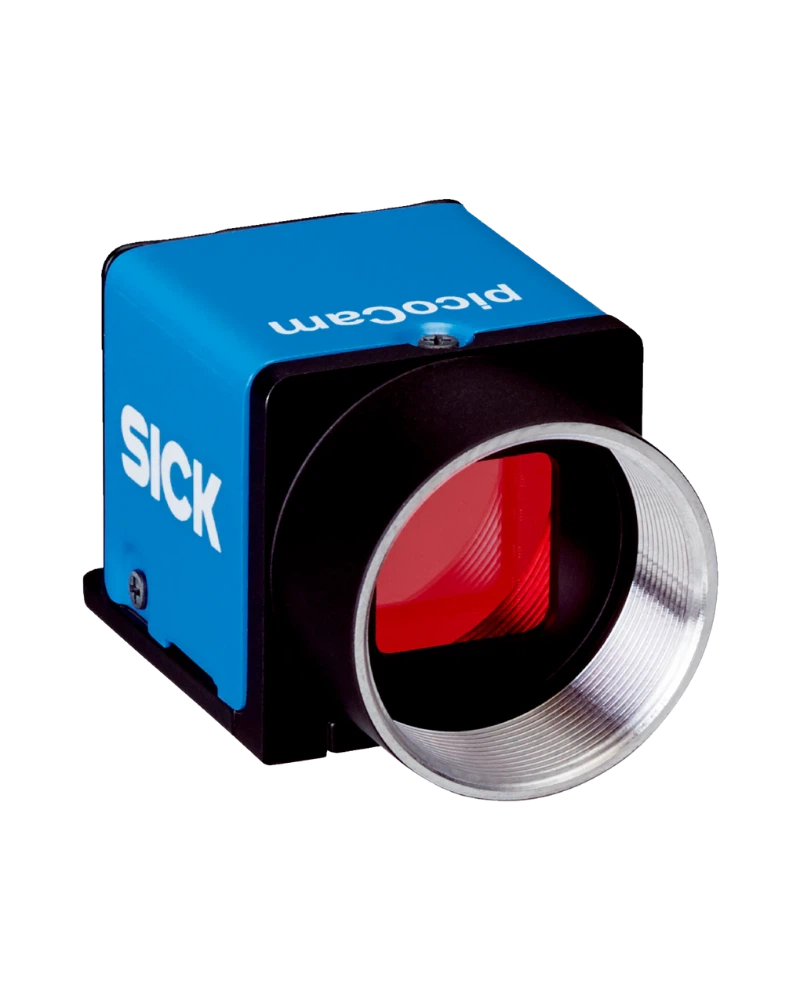
The SICK picoCam2 is a compact, high-performance machine vision camera designed for demanding industrial environments. It offers reliable image acquisition with flexible resolution options of 1, 3, or 5 megapixels in both color and monochrome variants. Built for integration into automated processes, the picoCam2 delivers consistent performance through robust industrial design and standardized connectivity. Its purpose is to support precise inspection tasks across a range of manufacturing applications where accurate visual data is essential. With proven use cases in industries such as food and beverage, automotive, and packaging, the picoCam2 enables efficient process control and quality assurance. The camera’s compact form factor and proven reliability make it ideal for integration into existing production lines without requiring major infrastructure changes.
The picoCam2 leverages industrial-grade connectivity to ensure stable communication in real-world settings. It features a screw-fit RJ45 GigE interface, which is the standard for industrial image processing, enabling high-speed data transfer and reliable network performance. This interface supports seamless integration with vision systems and control platforms. Additionally, the camera includes industry-grade plug connectors for voltage supply and trigger signals, simplifying installation and reducing potential points of failure. The combination of these features ensures robust operation in dynamic production environments. SICK’s technology is further demonstrated through real-world success stories such as its use at Nestlé, where deep learning and AI-driven process control have enhanced inspection accuracy and efficiency.
The picoCam2 offers resolution options of 1, 3, or 5 megapixels in both color and monochrome configurations. This flexibility allows users to select the appropriate image quality based on application requirements—balancing detail with processing speed. The camera is engineered for industrial use, featuring durable construction and optimized performance under varying conditions. Its GigE interface supports high-bandwidth data transmission, ensuring minimal latency during real-time inspection tasks. With a focus on reliability and ease of integration, the picoCam2 delivers consistent image quality across different lighting and operational scenarios. These technical specifications are designed to meet the demands of continuous production environments where precision and uptime are critical.
The picoCam2 is designed for straightforward configuration and integration into existing industrial systems. Its screw-fit RJ45 GigE interface enables direct connection to standard industrial vision networks, while industry-grade plug connectors simplify power and trigger signal connections. This modular design reduces setup time and enhances compatibility with a wide range of automation platforms. Users can easily select between 1, 3, or 5 megapixel resolutions in color or monochrome modes depending on their inspection needs. The camera’s standardized interfaces ensure compatibility with SICK’s ecosystem and third-party vision software, enabling rapid deployment without extensive customization.
The picoCam2 is engineered to operate reliably in industrial environments with typical temperature ranges and exposure to dust, vibration, and moisture. It is designed for use in continuous production settings where environmental conditions can vary. The camera’s robust construction ensures long-term performance under demanding operational conditions. While specific environmental ratings are not provided in the source material, its industrial-grade connectors and interface design indicate suitability for harsh environments common in manufacturing facilities. This makes it a dependable choice for applications requiring consistent operation over extended periods without maintenance.
The picoCam2 is ideal for a variety of industrial inspection tasks where high-resolution imaging is required. Its availability in both color and monochrome variants allows selection based on application needs, such as defect detection or alignment verification. It has been successfully deployed in applications like process control at Nestlé, where deep learning techniques enhance quality assurance through intelligent image analysis. The camera supports use in food and beverage, automotive, and packaging industries for tasks including product inspection, dimensional measurement, and presence/absence detection. Its reliable performance and flexible configuration make it a versatile solution across diverse manufacturing environments.
| Specification | Value |
|---|---|
| resolution | in color and monochrome variants. CMOS image sensors use global shutter technology and enable multiple image sections (AOI). Image recording and transmission are decoupled in the internal 126 MB memory bank, meaning multi-camera applications are supported. |
Browse product families and jump into the exact catalog section you need.