Explore performance details, construction highlights, applications, and technical information in one clear overview.
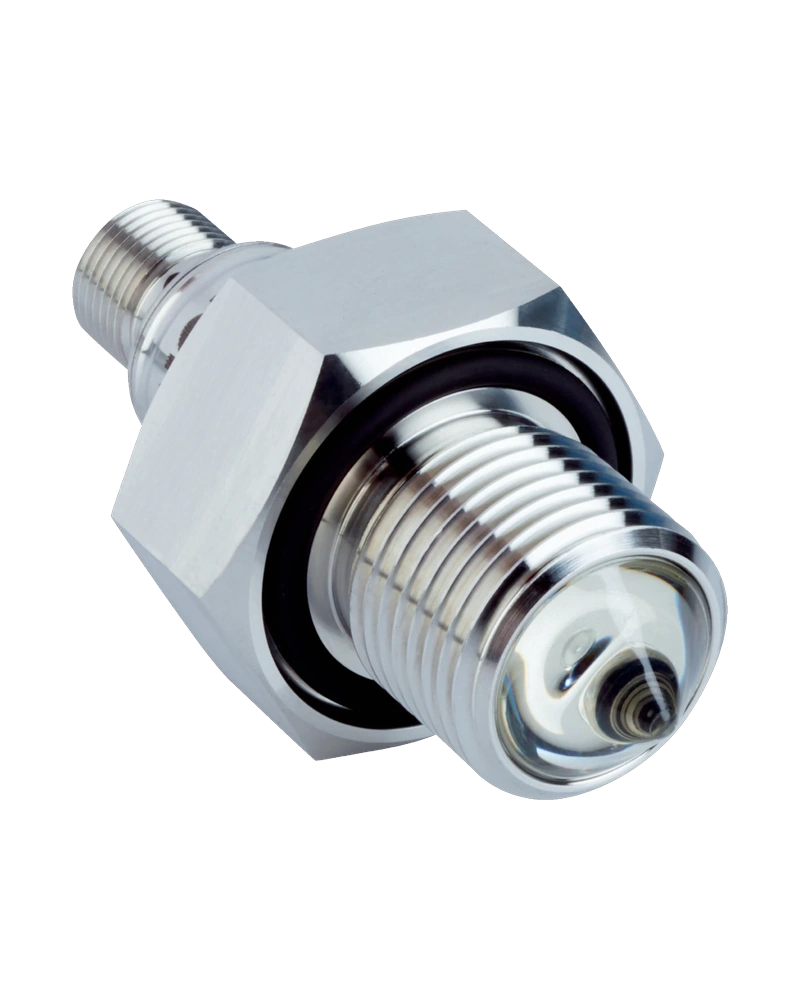
The GRF18S is a robust level switch sensor designed for reliable detection of liquid levels in industrial processes. Utilizing visible red LED technology, it provides accurate on/off switching to indicate whether the process medium has reached a specific level. With a compact and durable stainless steel housing, the GRF18S ensures long-term performance in demanding environments. Its normally closed switching mode delivers immediate feedback when the liquid level is detected or absent. The sensor operates within a wide pressure range of –0.5 bar to 20 bar and supports ambient temperatures from –10 °C to +55 °C, making it suitable for diverse industrial applications. Designed with safety in mind, the GRF18S meets protection class III standards and is fully protected against overcurrent and short circuits, ensuring safe operation under all conditions.
The GRF18S employs a visible red LED light source to detect liquid levels through optical sensing. This technology ensures reliable detection even in challenging media with minimal interference from ambient light or process conditions. The sensor features a fast response time of 10 ms, enabling quick reaction to level changes. It is constructed from stainless steel 1.4404 / 316L, offering excellent corrosion resistance and durability. The normally closed switching mode ensures a secure default state when no liquid is present. With a maximum switching frequency of 250 Hz, the sensor can handle rapid level fluctuations without signal degradation. Its LED-based design provides consistent performance over time, while being energy-efficient and resistant to environmental influences such as dust or moisture.
The GRF18S operates within a supply voltage range of 10 V DC to 30 V DC with reverse polarity protection and U V connections. Residual ripple is limited to ≤5 V pp, ensuring stable signal output. The sensor outputs a single PNP signal with an output current of ≤100 mA, protected against overcurrent and short circuits. It features a G ½ process connection for direct integration into tanks or vessels. The housing is rated IP67 and IP69, providing full protection against dust ingress and temporary immersion in water up to 1 meter deep. The enclosure is built from stainless steel 1.4404 / 316L, ensuring resistance to corrosion and mechanical stress. All specifications are designed for consistent performance under industrial conditions.
The GRF18S integrates seamlessly into existing process systems via a standard M12 round connector with four pins. No additional communication interface is required, as it provides a simple PNP output signal suitable for direct connection to control systems or PLCs. The sensor’s normally closed switching mode ensures safe default behavior when no liquid is detected. Reverse polarity protection and U V tolerance compliance ensure safe operation even under electrical stress. Installation requires only a G ½ process connection to the vessel, enabling straightforward setup in tanks, silos, or other level monitoring applications. No external power supply or signal conditioning is needed—just a stable DC voltage between 10 V DC and 30 V DC.
The GRF18S is designed for operation within ambient temperatures ranging from –10 °C to +55 °C. It can be stored in environments from –25 °C to +70 °C, allowing flexibility during transport and installation. The sensor withstands process conditions of –0.5 bar to 20 bar pressure, making it suitable for both vacuum and high-pressure applications. Its IP67 and IP69 ratings ensure complete dust tightness and resistance to temporary immersion in water or high-pressure washdowns. These environmental capabilities make the GRF18S ideal for use in harsh industrial settings such as chemical processing, food & beverage, and pharmaceutical manufacturing where exposure to moisture, dust, or pressure fluctuations is common.
The GRF18S is well-suited for level monitoring in a variety of industrial processes including liquid storage tanks, process vessels, and silos. Its reliable switching action and robust construction make it ideal for use in food & beverage, chemical, pharmaceutical, and water treatment industries. It can detect the presence or absence of liquids in closed systems with minimal maintenance. The sensor’s resistance to corrosion and ability to operate under varying pressure conditions ensures consistent performance across different media types. With no communication interface required, it simplifies integration into existing control systems without additional wiring or software configuration.
| Specification | Value |
|---|---|
| Light source | LED |
| Response time | 10 ms |
| Communication interface | - |
| Supply voltage | 10 V DC ... 30 V DC 1) |
| Protection class | III |
| Connection type | M12 round connector x 1, 4-pin |
| Switching frequency | 250 Hz 4) |
| Housing material | Stainless steel 1.4404 / 316L |
| Ambient temperature | , storage |
| Process pressure | –0.5 bar ... 20 bar |
| value | IP67 IP69 |
| Process temperature | –10 °C ... +55 °C |
| Residual ripple | ≤ 5 V pp 2) |
| Output signal | 1 x PNP 3) |
| Output current | ≤ 100 mA Output overcurrent and short-circuit protected |
| Enclosure rating | IP67 IP69 |
| Process connection | G ½ |
| Ambient operating temperature | –10 °C ... +55 °C |
| Ambient temperature, storage | –25 °C ... +70 °C |
| Unit weight | 0.144 Kilograms |
| Net unit weight | 0.144 Kilograms |
| M12 round connector x | 1, 4-pin |
| IP67 | IP69 |
Browse product families and jump into the exact catalog section you need.