Explore performance details, construction highlights, applications, and technical information in one clear overview.
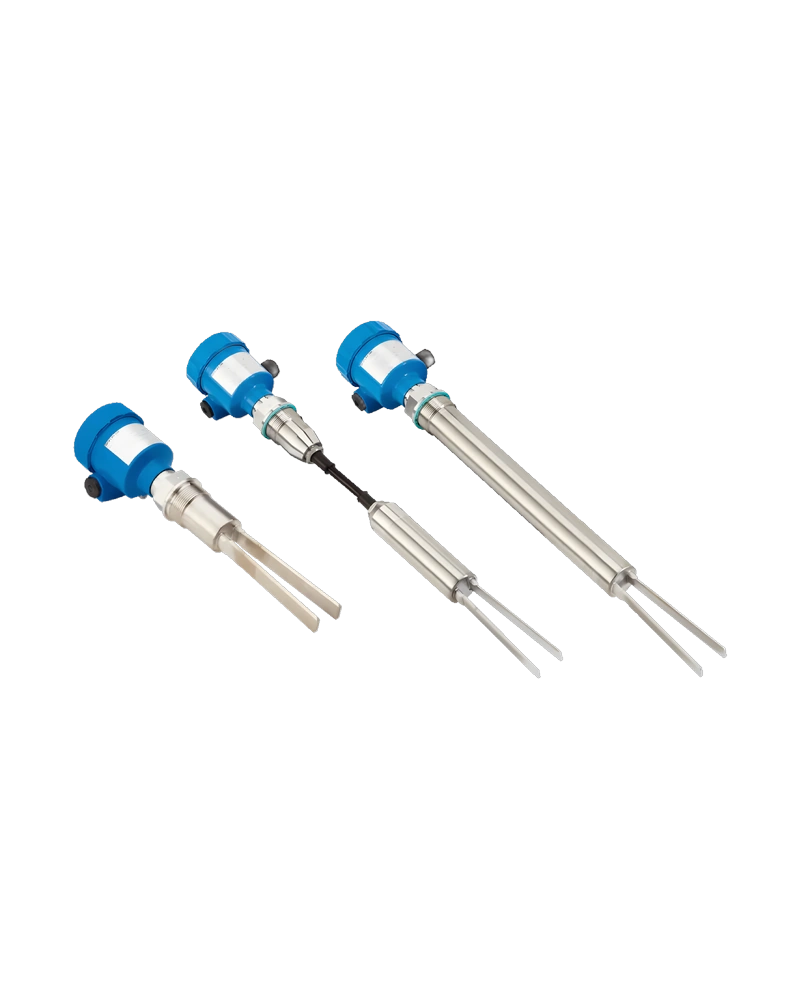
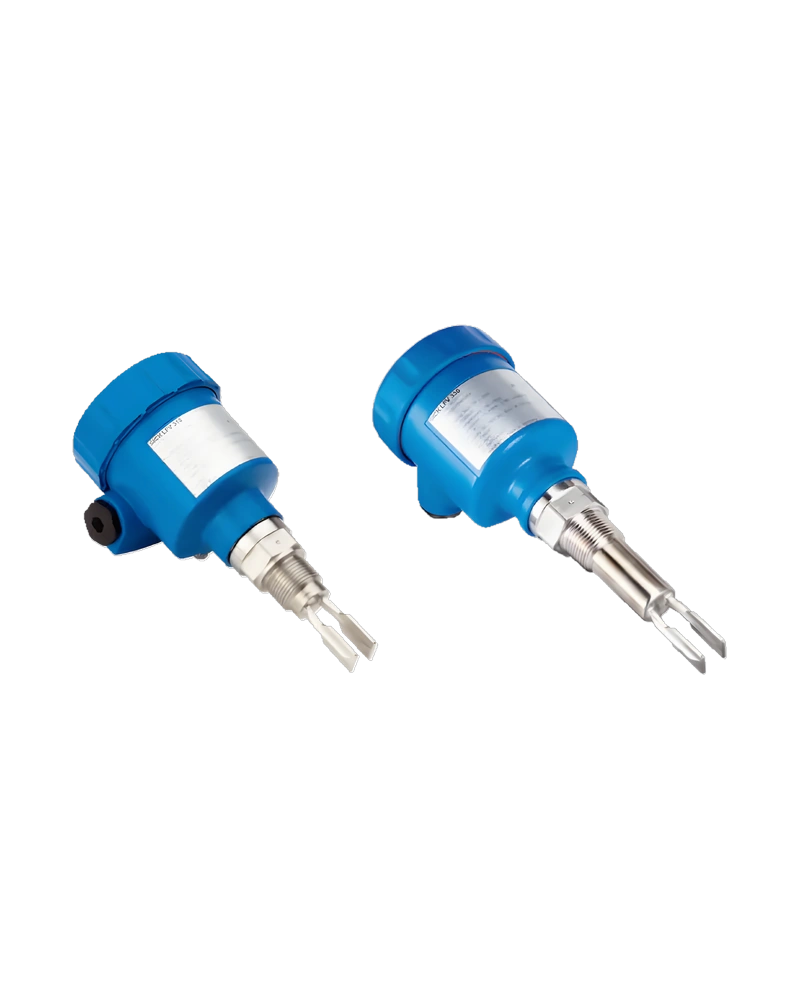
The LBV300 is a vibrating level switch designed for reliable detection of bulk materials in industrial processes. It operates by sensing changes in vibration amplitude when material covers the internal vibrating rod or fork, enabling accurate determination of full, empty, or demand conditions. The sensor is maintenance-free and certified ATEX-approved, making it ideal for use in hazardous environments including those involving explosive atmospheres. Additionally, its suitability for foodstuffs ensures compliance with hygiene standards in food processing applications. With a proven track record in demanding industrial settings, the LBV300 delivers consistent performance without requiring regular servicing or calibration.
The LBV300 utilizes vibrating rod technology to detect material presence. As bulk material comes into contact with the vibrating component, it alters the vibration amplitude, which is immediately sensed by the device. This change triggers a reliable switching signal indicating whether the level is full, empty, or at a specific demand point. The sensor's operation is fully automatic and requires no mechanical parts to be replaced, ensuring long-term reliability. Its design ensures robust performance in challenging conditions, including high dust or particulate environments. The technology provides fast response times and consistent detection accuracy across various material types, making it suitable for both static and dynamic bulk handling scenarios.
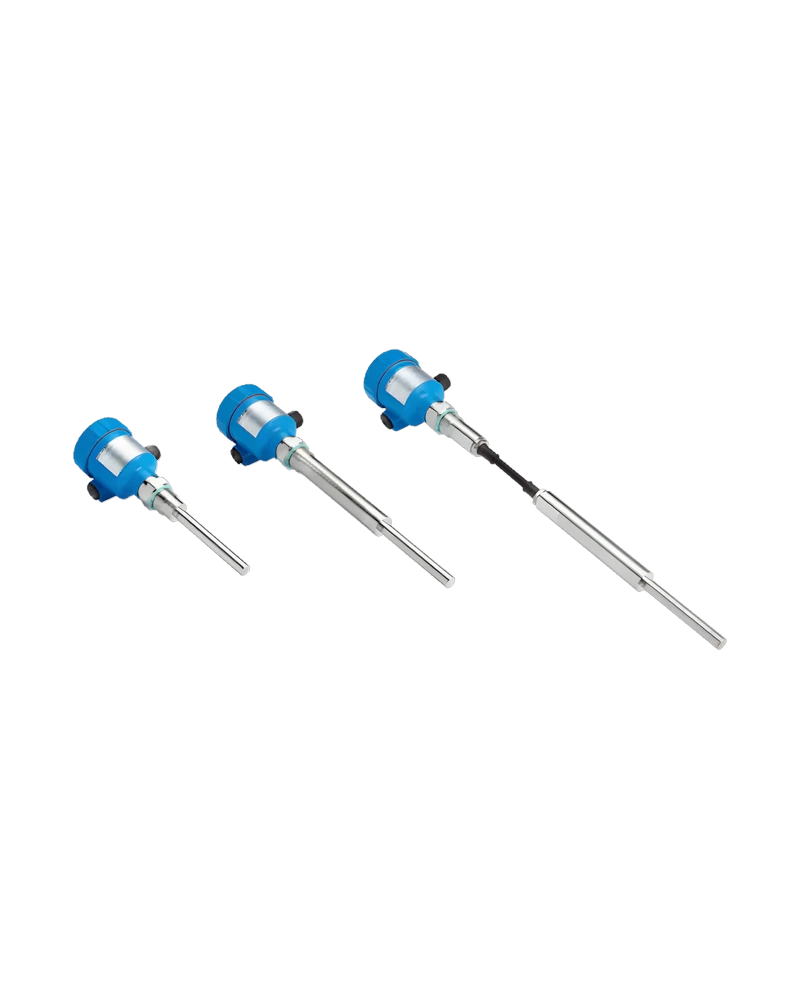
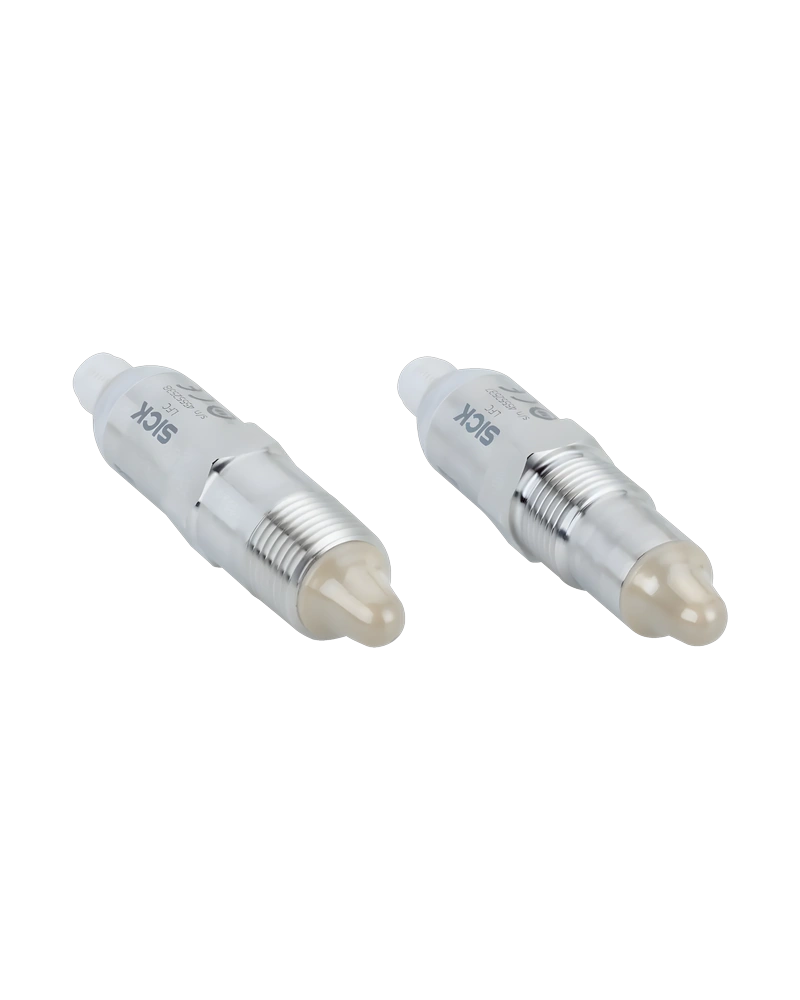
The LBV300 is part of the LBV3xx series, offering a range of sensing solutions tailored to different installation needs. While the compact LBV31x model supports lateral mounting, the extended LBV33x tube design provides vertical mounting options with sensing ranges up to 6 meters. The sensor detects changes in vibration amplitude when material covers the vibrating rod or fork, translating this physical change into a clear switching signal. It is specifically engineered for use in bulk materials and is certified ATEX-approved for operation in explosive atmospheres. Its construction ensures durability and performance under varying process conditions, with no need for maintenance during service life.
The LBV300 offers a wide range of process connections and multiple electronic variants to suit diverse application requirements. This flexibility allows integration into various control systems and process environments, including those with hazardous gas or dust conditions. The availability of different connection types ensures compatibility with standard industrial piping and equipment setups. With support for both lateral and vertical mounting configurations—depending on the model variant—the sensor can be adapted to fit specific installation constraints. Its ability to generate a reliable switching signal makes it easily compatible with PLCs, SCADA systems, or other automation platforms used in process control.
The LBV300 is designed for operation in harsh industrial environments, including those with explosive atmospheres. It is ATEX-approved, ensuring safe use in potentially hazardous areas such as chemical processing, mining, or food manufacturing. The sensor performs reliably across a range of temperatures and humidity levels typical in bulk material handling applications. Its maintenance-free design ensures long-term stability without degradation due to environmental exposure. The device is suitable for use with foodstuffs, meeting hygiene requirements necessary in food processing environments. It can be deployed in both clean and dirty conditions, provided the material does not interfere with the internal vibrating components.
The LBV300 is widely used as a full, empty, or demand detector in bulk material handling systems across multiple industries. Its reliable detection mechanism makes it ideal for applications such as silo level monitoring, tank level control, and process inventory management. The sensor's ATEX certification enables safe deployment in hazardous areas, while its food-grade suitability supports use in pharmaceuticals and food processing. Whether used vertically or laterally, the LBV300 provides accurate, maintenance-free detection across a range of materials including powders, granules, and bulk solids. Its compatibility with various process connections ensures seamless integration into existing industrial automation systems.
| Specification | Value |
|---|---|
| material | covers the vibrating rod or fork, the vibration amplitude changes. The sensors reliably detect this change and convert it into a switching signal. The products can also be used in the food industry. While the LBV31x compact device is suitable for lateral mounting, the LBV33x tube-extended sensor with |
| sensing range | s of up to 6 m is used for vertical mounting. With a wide range of process |
| connection | s and several electronic variants, LBV3xx offers a solution for numerous applications, even in explosive atmospheres. |
Browse product families and jump into the exact catalog section you need.